No.0 Plating Barrel Bending Machine
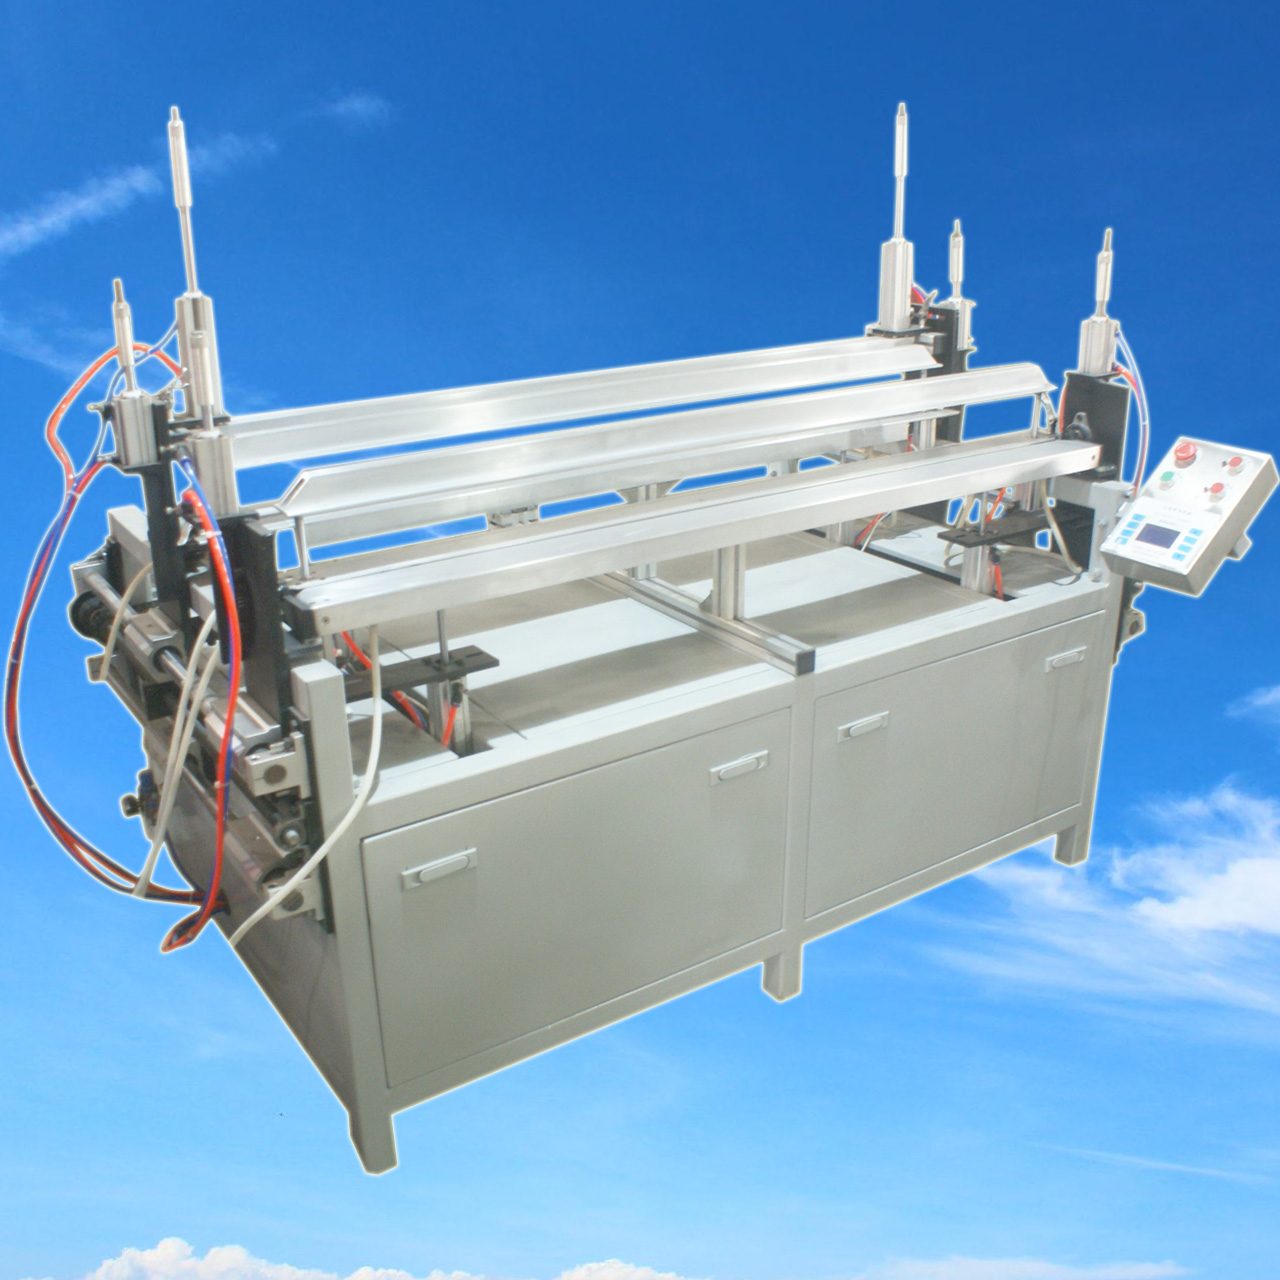
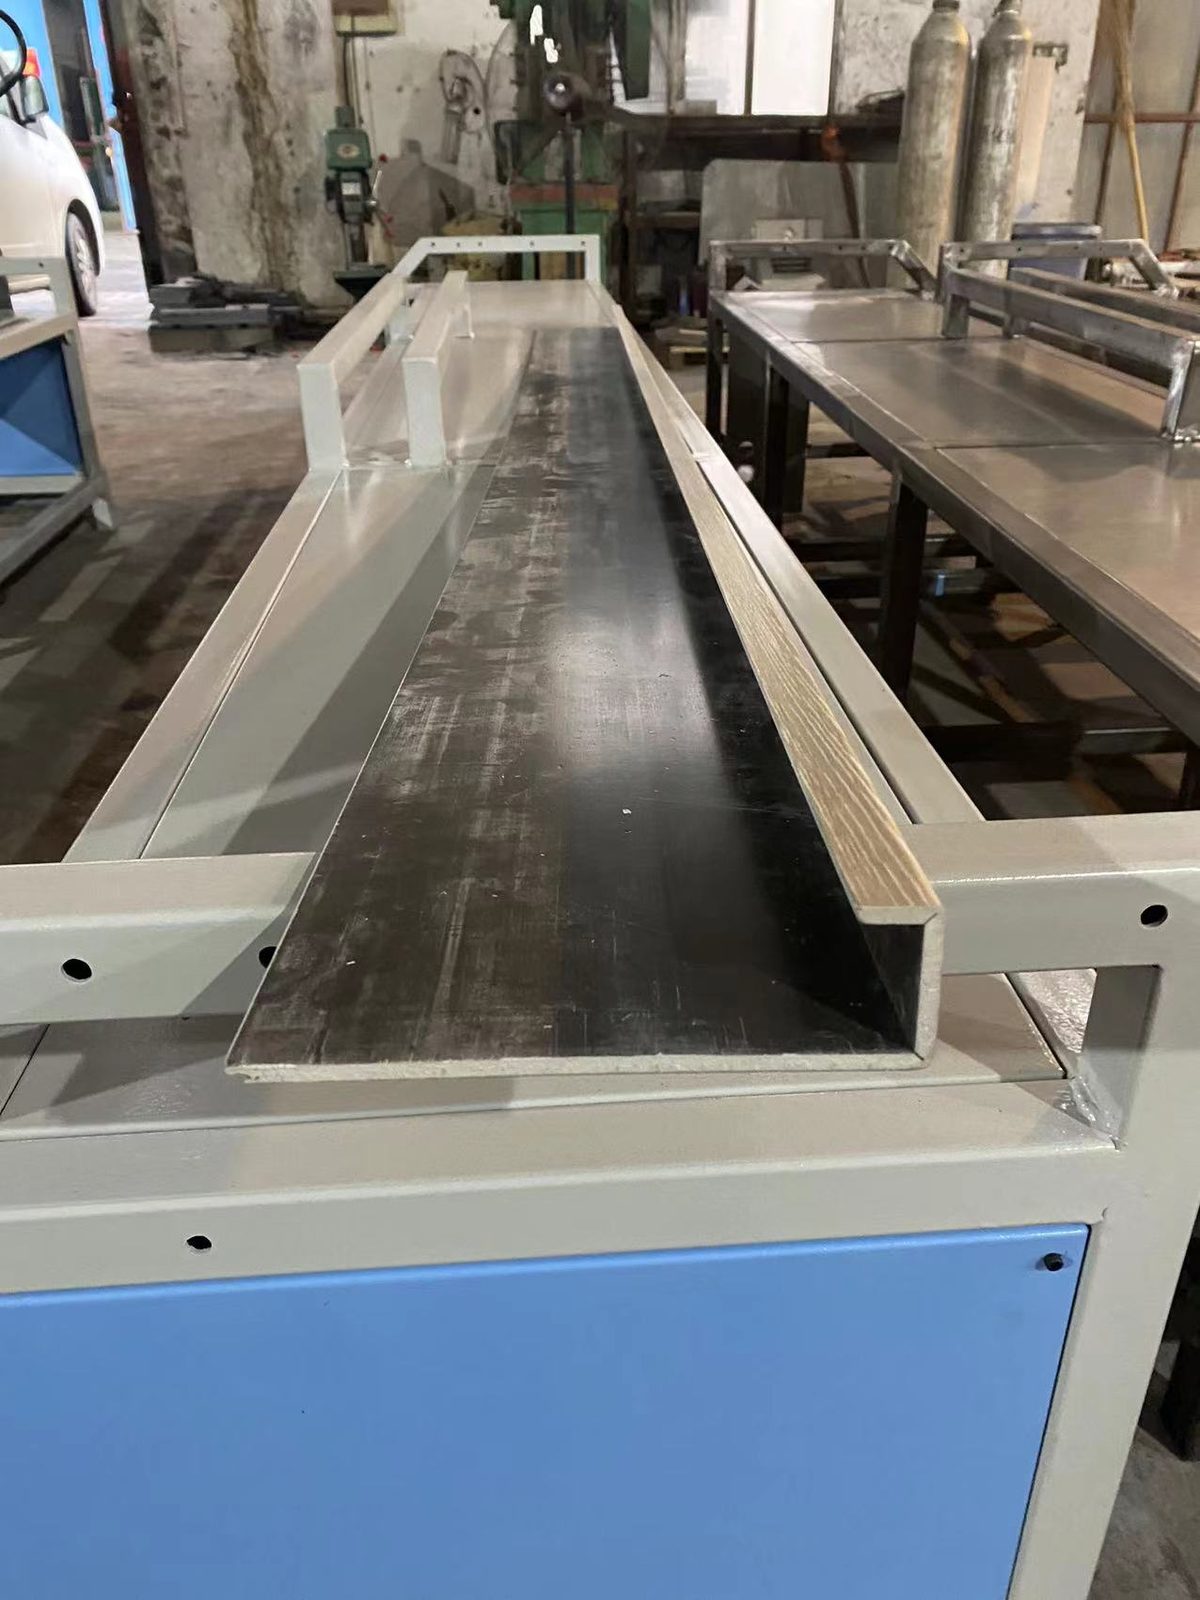
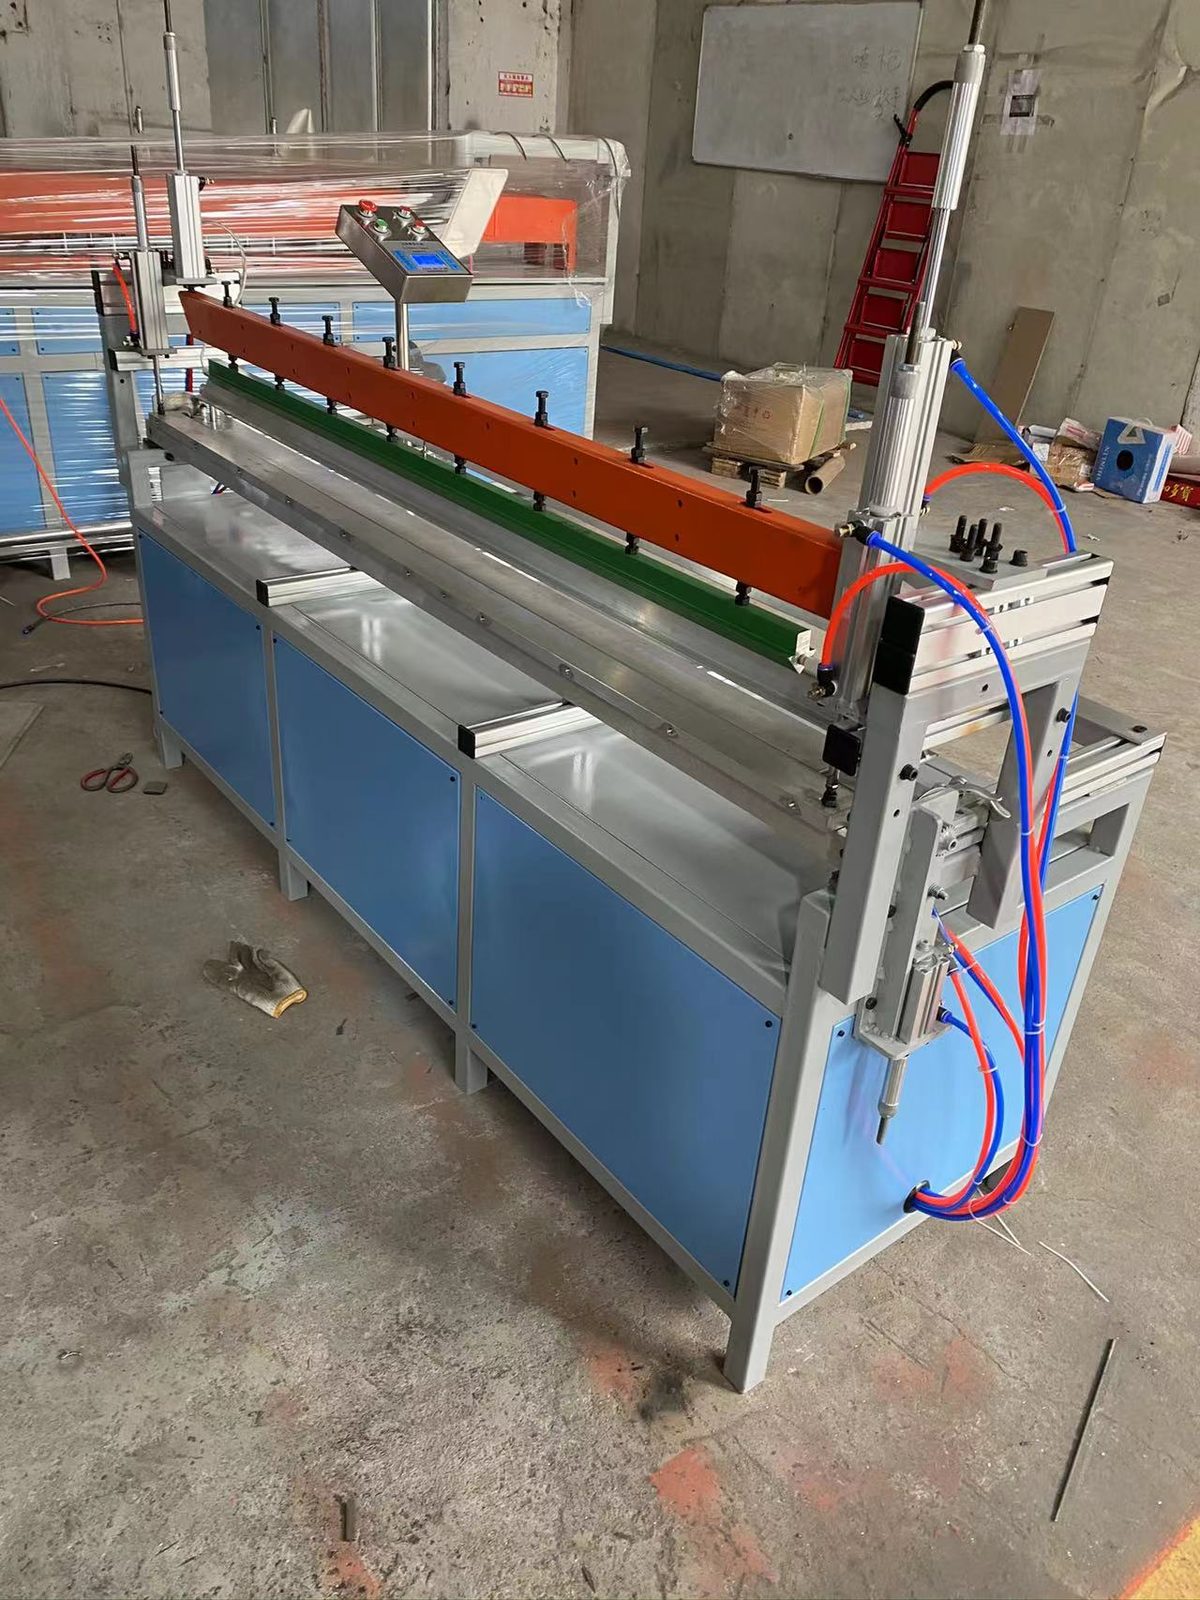
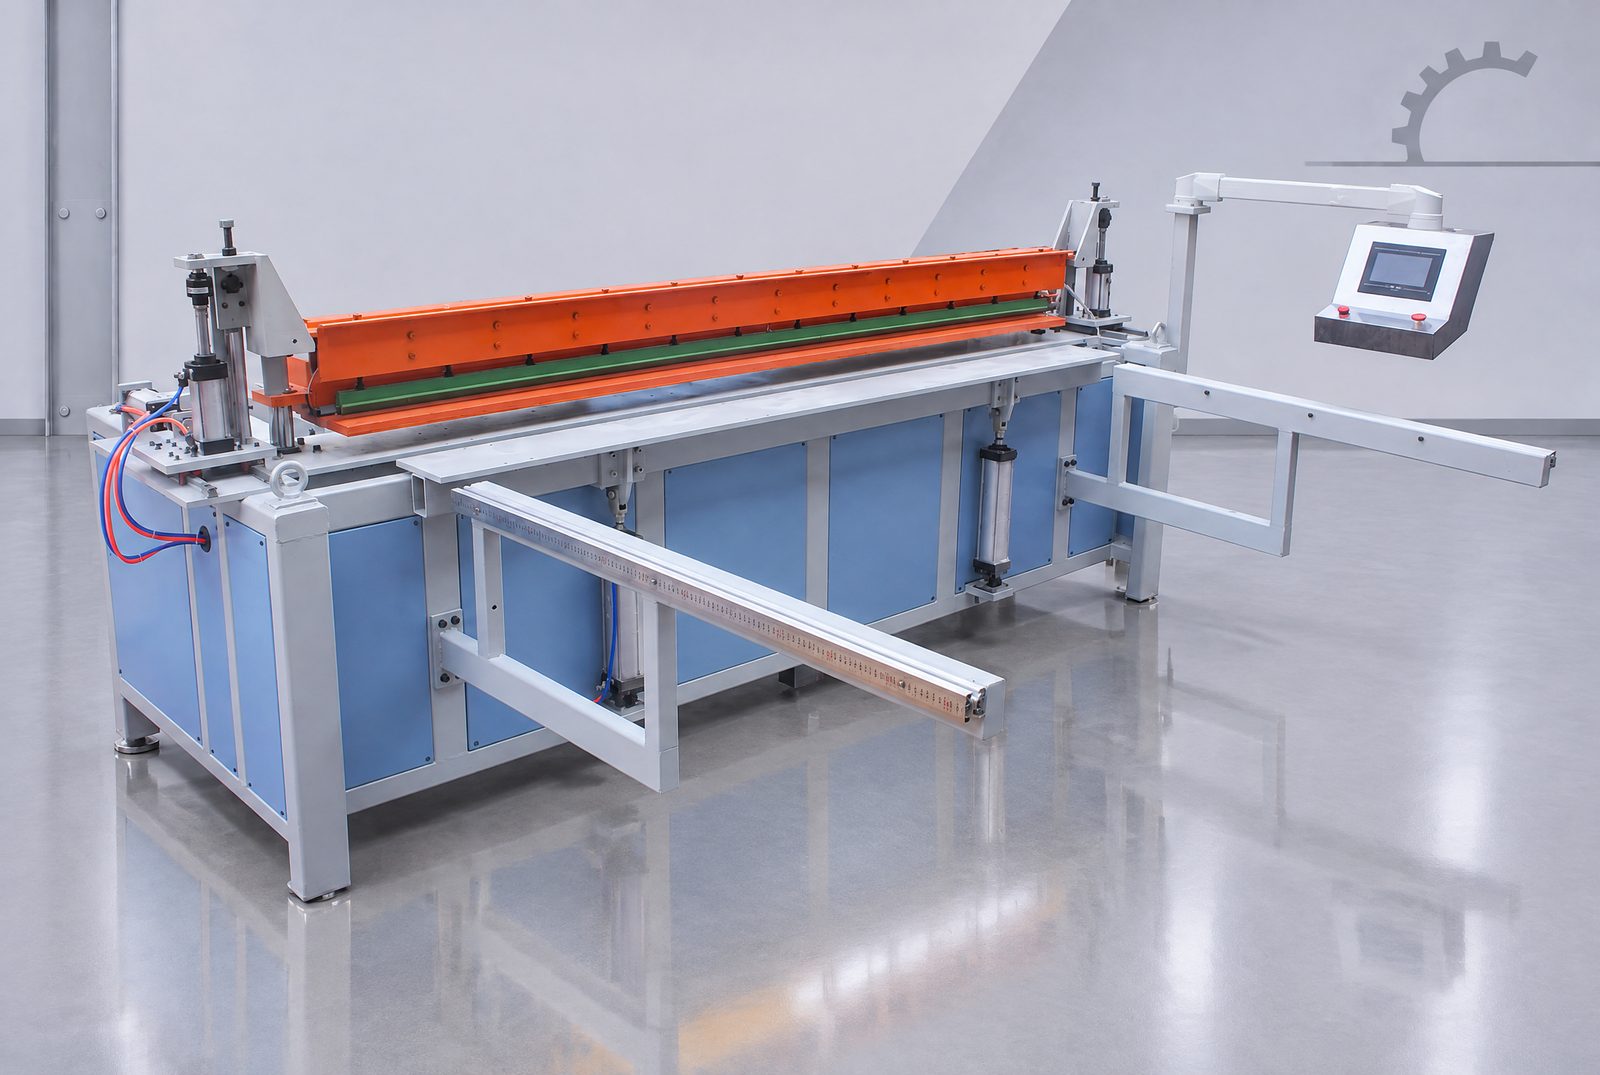
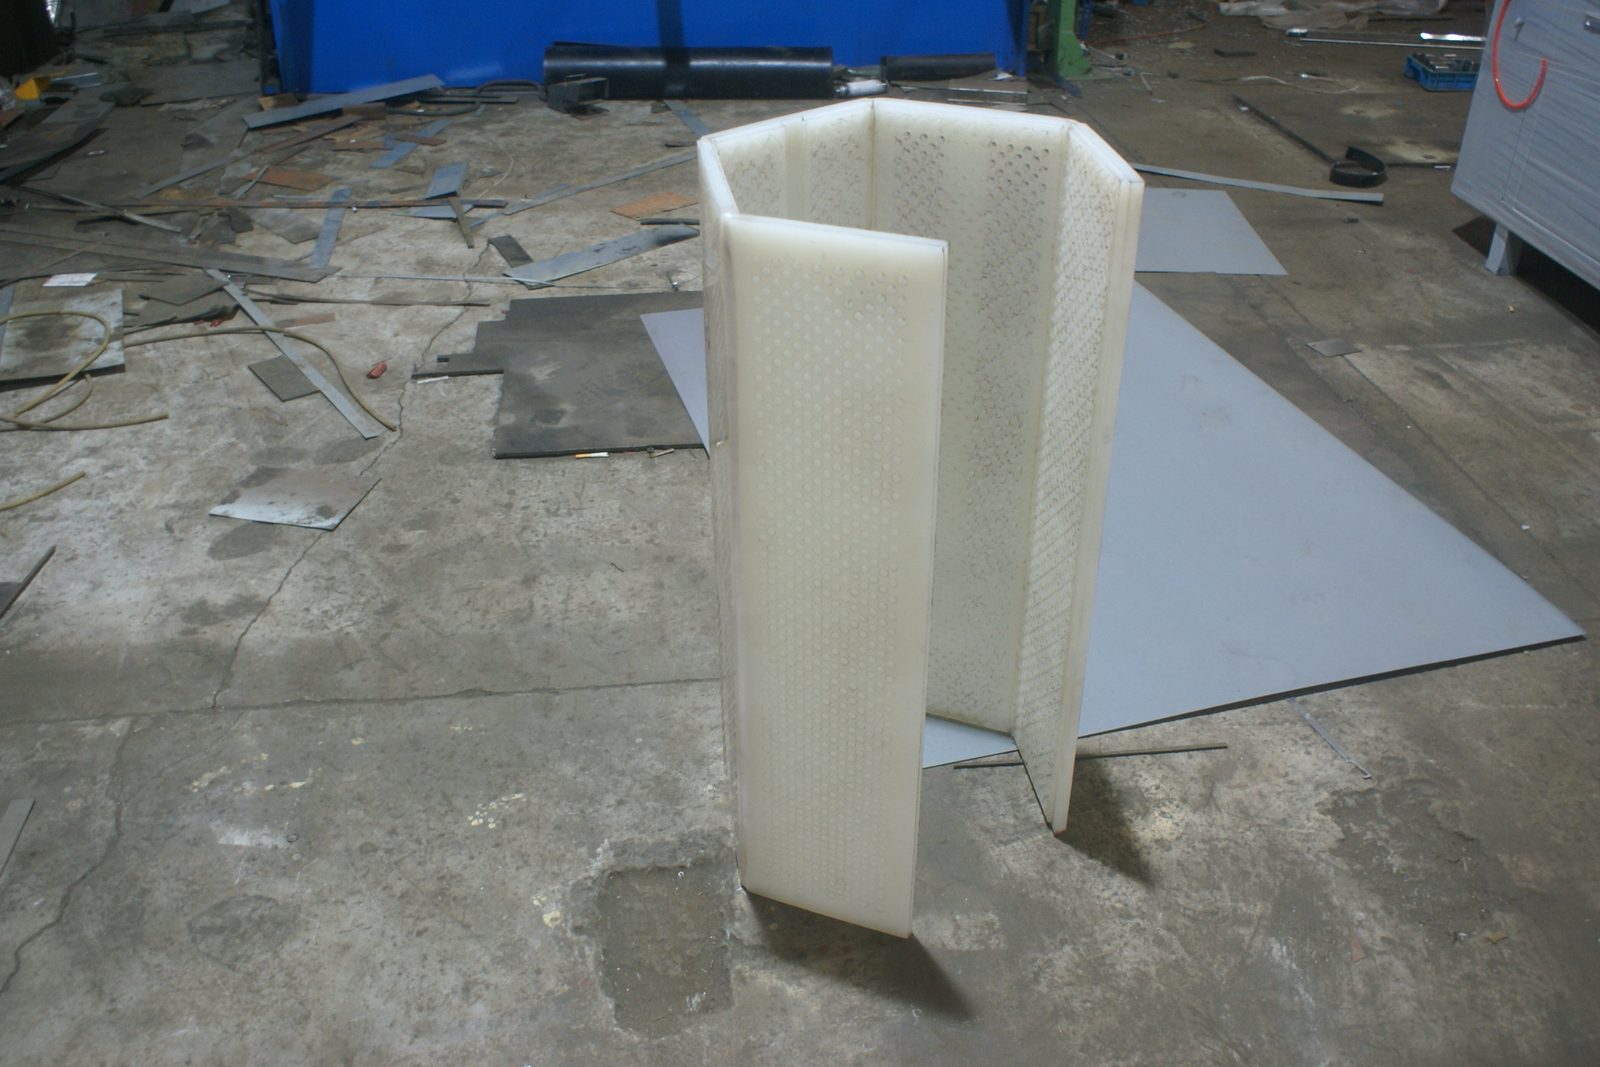
One PP sheet is folded into a polygonal barrel — 120° per face for a hexagon, 135° for an octagon. The barrel closes with a single longitudinal seam instead of six.
What it solves
01Every welded seam is where plating solution starts to seep.
Hand-welded barrels lose concentricity and run out of true.
Seams must be polished, and the inner wall is the hardest place to reach.
Core value
02One sheet, one seam.
Concentric barrels that run true.
Five fewer seams to grind.
How it works
03- 01Face-by-face folding
The sheet is fed and bent at the set angle, face after face.
- 02Closed-form accuracy
Servo feed keeps every face the same length, so the last seam lines up.
- 03Fewer seams, fewer leaks
One longitudinal weld instead of six.
- 04Buffered stroke
Thick sheet folds without cracking, keeping barrel strength.
Specifications
04| Sheet thickness | up to 25 mm (0.98 in) |
|---|---|
| Bending length | 1500–5000 mm (4.9 ft–16.4 ft) |
| Bending angle | 60°–180°, adjustable |
| Barrel forms | hexagonal / octagonal / polygonal |
| Power | 6–14 kW |
| Voltage | 380 V / 50 Hz |
Advantages
05Barrel forming
- Hexagon at 120°, octagon at 135°, face by face.
- One sheet, one revolution, one seam.
- Concentricity comes from the program, not from the welder.
Control
- CNC feed keeps every face equal.
- Barrel presets stored; change form by changing face count and angle.
- Buffered stroke for thick sheet.
What it bends
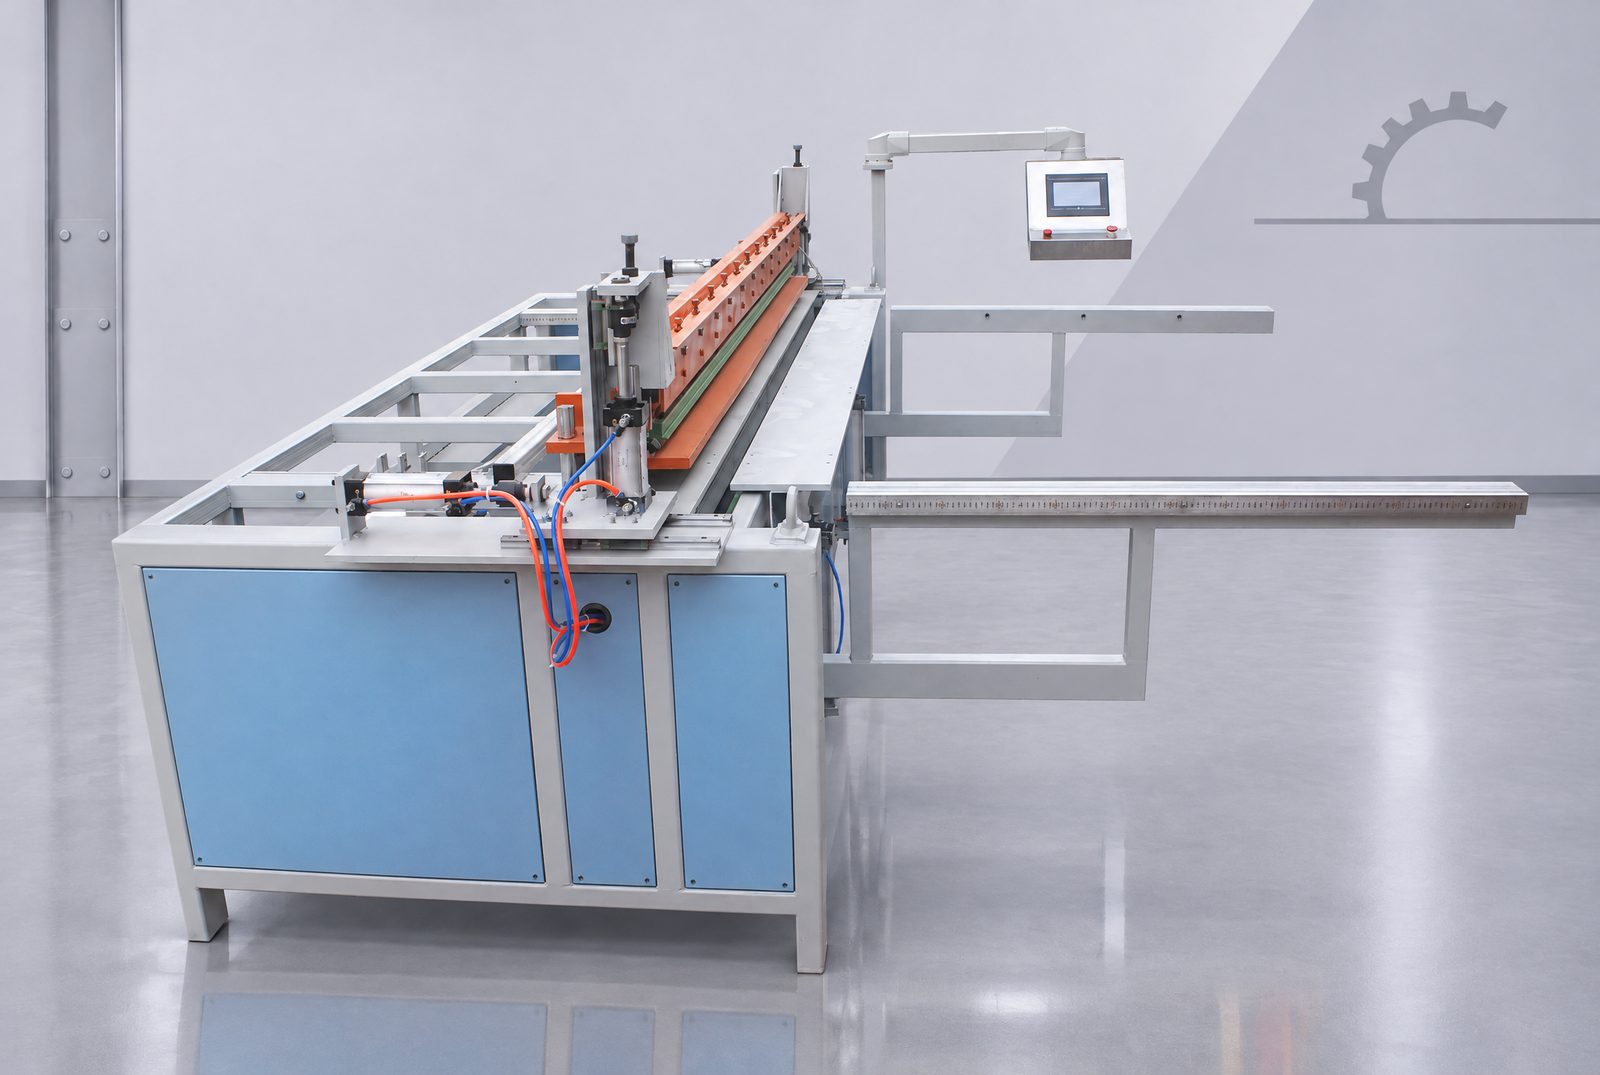
06Machine detail
Video
Post a 200 × 200 mm offcut with material and thickness noted; we bend it to your angle and send photos plus video within 48 hours.
Request a trial bendAlso known as
07All names above refer to this machine — see the full alias index.
FAQ
08How many folds does one barrel need?
Six for a hexagonal shell, eight for an octagonal one — each barrel closes with one longitudinal seam.
What about concentricity?
Servo feeding keeps every face the same length, so the shell runs true.